Custom Plastic Injection Molding Services
Know your part before you tool it. We manufacture custom plastic parts to your CAD, with low-MOQ production and a minimum quantity confirmed for your part, material and tooling requirements
- Free DFM in 4 Hours, Firm Quote in 24 Hours
- First Samples in 3 Days, No Tooling Cost
- Certified Plastic Parts Tolerance: ±0.002″ (±0.05 mm)
Get an Injection Molding Quote in 24 Hours
Get pricing for your custom injection molded parts
Your files are secure and confidential
10+
Years in Business
800K
Pcs / Month
70%+
Repeat Clients
98%
On-Time Delivery
ISO
9001 · BSCI
HM Manufacturing has achieved an on-time delivery rate of up to 98% for more than 3,600 customers
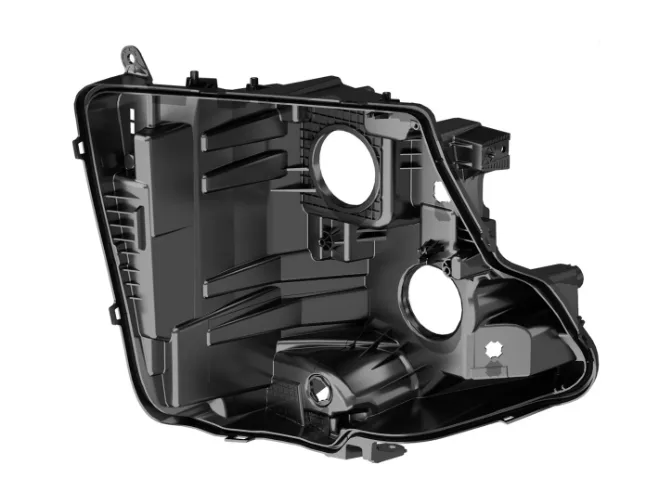
Injection Molding
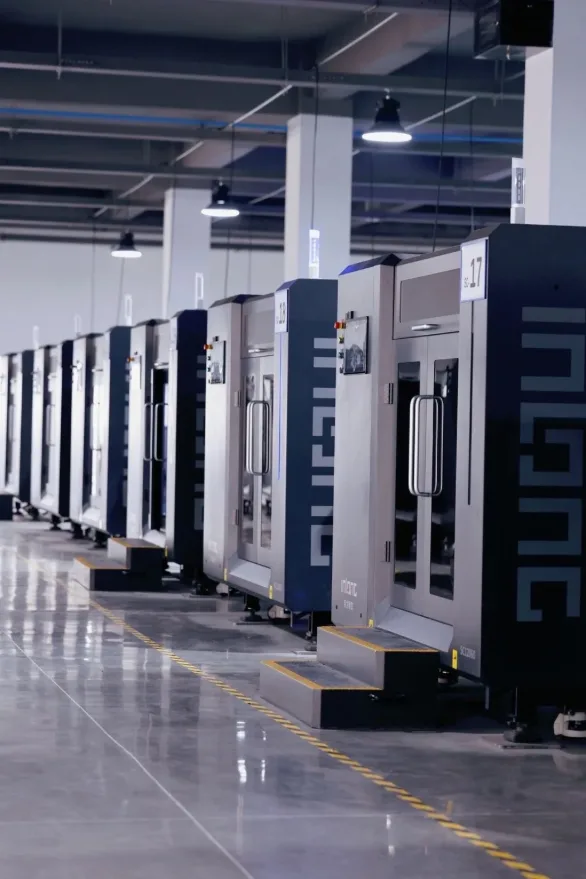
High-volume production in food-grade and engineering resins, from 500 to 1M+ parts on one steel tool with tight, repeatable tolerances
Tolerance± 0.002″Cavities1–64Lead Time15–25 daysMOQ500 pcs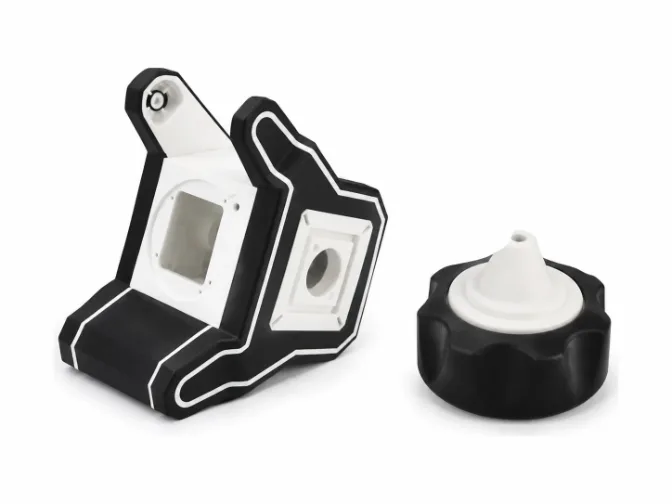
Overmolding
Soft-touch TPE and TPU over ABS, PC and nylon substrates for grips, seals, cable assemblies and durable multi-material housings
SubstratesABS, PC, PAShore Hardness20–90 ALead Time20–30 daysMOQ500 pcs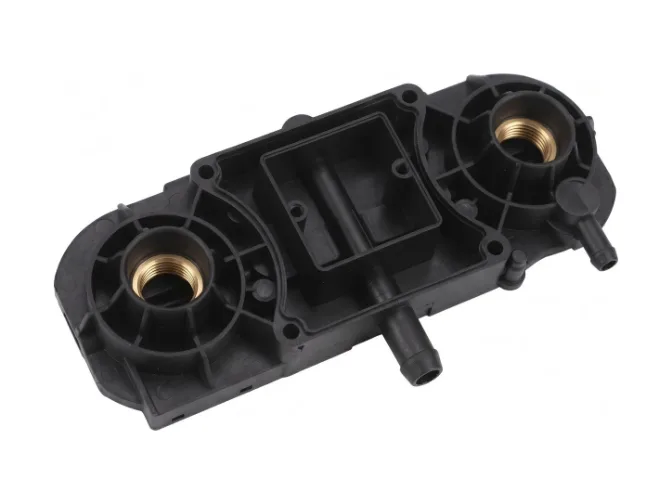
Insert Molding
Brass and stainless inserts, threaded bushings and metal contacts molded into plastic in one shot for strong, reliable assemblies
Insert SizeM2–M12Insert Position± 0.002″Lead Time20–35 daysMOQ500 pcs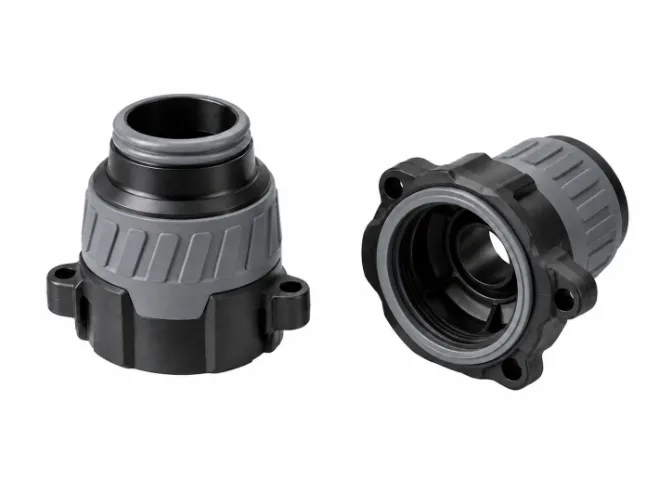
Two-Shot Injection Molding
Two resins or colors bonded in a single cycle for hard-soft grips, sealed housings and multi-color parts, with no secondary assembly
Method2 resins / cycleTolerance± 0.002″Lead Time25–40 daysMOQ1,000 pcs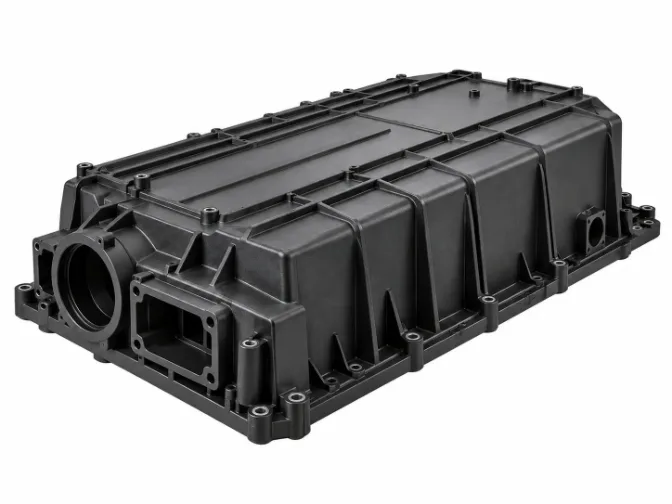
Large Part Injection Molding
Large enclosures and structural parts on high-tonnage presses, with wall-thickness and warpage control for stable dimensions across long runs
Clamp Forceup to 2,000 TShot Weightup to 5 kgLead Time20–35 daysMOQ300 pcs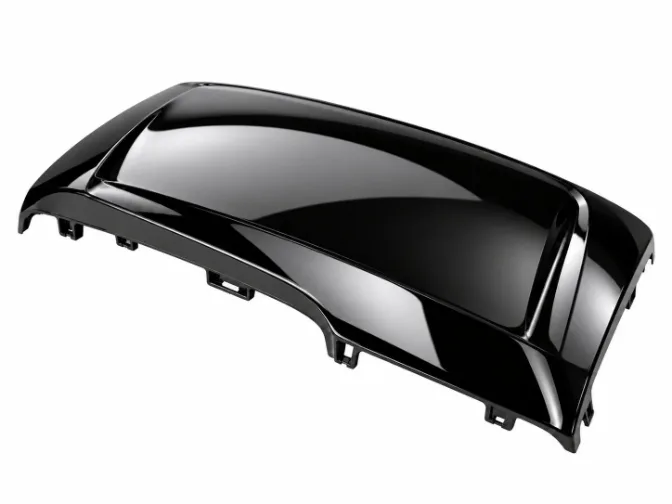
High-Gloss Injection Molding
Class-A, mirror-finish surfaces for visible housings and consumer products, using polished tooling and tightly controlled process windows
SurfaceSPI A1–A2Gloss90+ GULead Time20–30 daysMOQ500 pcs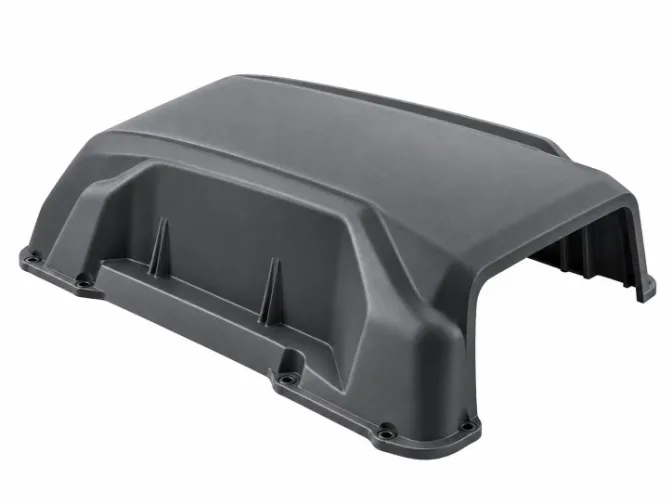
Reaction Injection Molding (RIM)
Low-pressure polyurethane RIM for large, lightweight enclosures with thick walls, foam cores and integrated ribs at low tooling cost
Wall Thickness3–25 mmPart Sizeup to 1.5 mLead Time15–25 daysMOQ100 pcs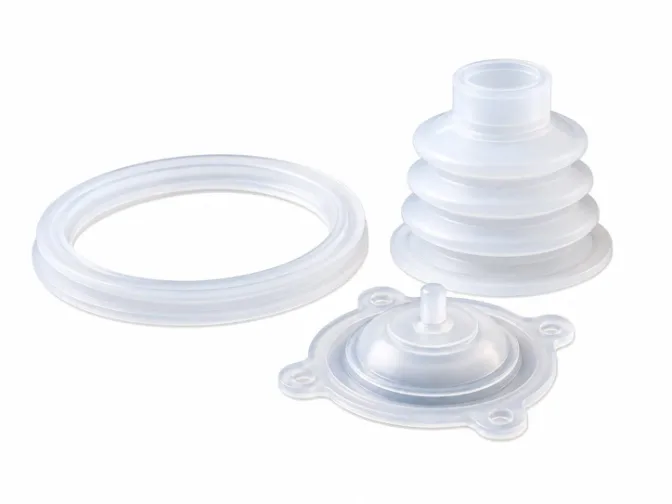
Liquid Silicone Rubber Molding (LSR)
Biocompatible LSR for seals, gaskets and soft parts that resist heat, chemicals and repeated flexing, for medical and consumer goods
Shore Hardness10–80 ATolerance± 0.05 mmLead Time20–30 daysMOQ1,000 pcsInjection Molding Materials
We run a broad range of engineering thermoplastics, elastomers and composites in-house. Our material options support ABS injection molding, PC injection molding and PP injection molding for common housings and functional parts, plus TPE injection molding, Tritan injection molding and PPSU injection molding for flexible, clear or heat-resistant applications. Tell us your mechanical, thermal and regulatory targets and we'll match the right resin to your part — from prototype to production
Colours, finishes, price bands and lead times shown are typical references and are confirmed on your quotation
Injection Mold Surface Finishes
We offer SPI surface finishes for your injection molds, from SPI A1/A2/A3 mirror grades to a matte injection molding finish. Our injection molding expert helps you choose the right finish — upload your design on our quoting platform and get a detailed quote within 24 hours
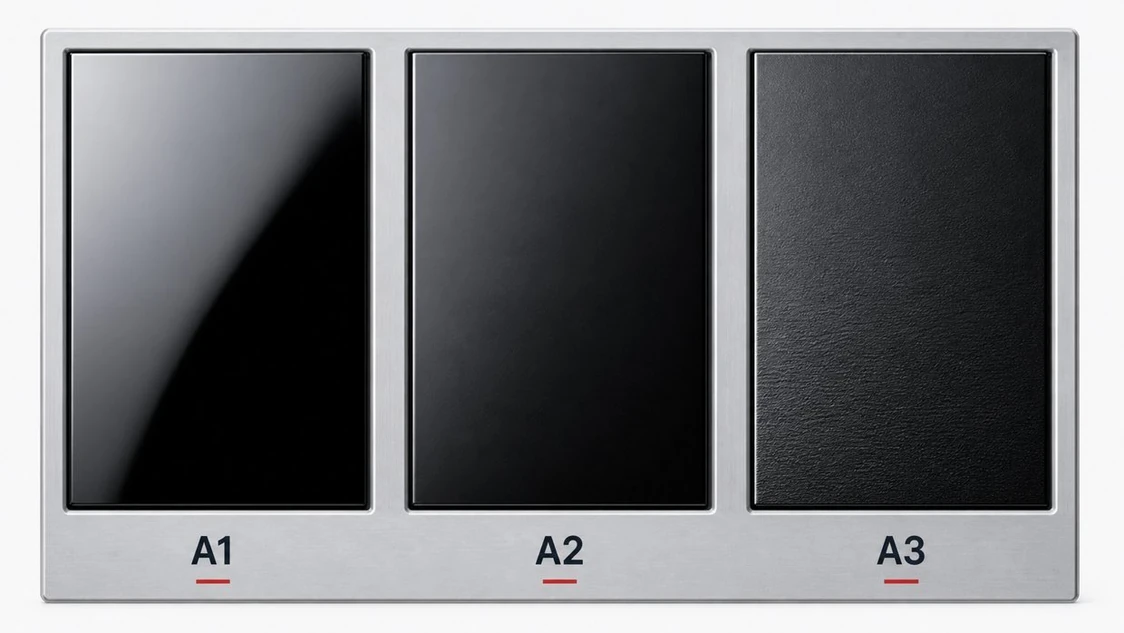
SPI A
Ra 0.012 – 0.10 µmMirror to high-gloss finishes for parts where appearance is critical
| Grade | Ra (µm) | Method | Best for |
|---|---|---|---|
| A1 | 0.012 – 0.025 | 6000# diamond | Optical lenses; zero-defect parts |
| A2 | 0.025 – 0.05 | 3000# diamond | Clear housings; premium goods |
| A3 | 0.05 – 0.10 | 1200# diamond | General cosmetic gloss parts |
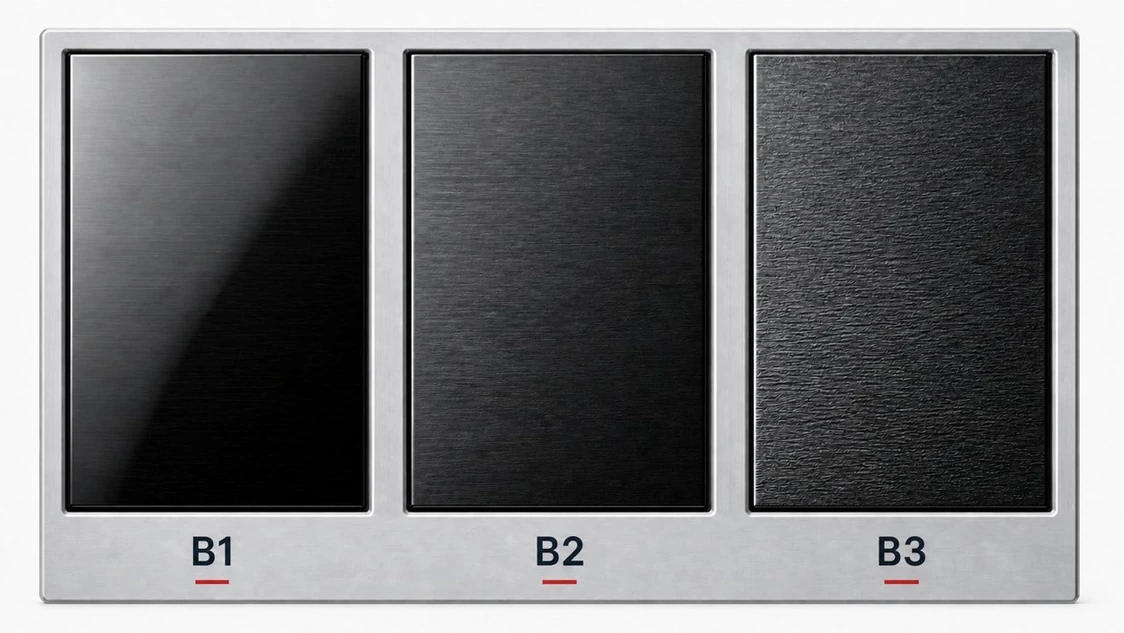
SPI B
Ra 0.05 – 0.28 µmSemi-gloss finishes that balance looks with everyday durability
| Grade | Ra (µm) | Method | Best for |
|---|---|---|---|
| B1 | 0.05 – 0.10 | #600 paper | Fingerprint-hiding surfaces |
| B2 | 0.10 – 0.20 | #400 paper | Auto interiors; electronics |
| B3 | 0.20 – 0.28 | #320 paper | Smooth-feel budget parts |
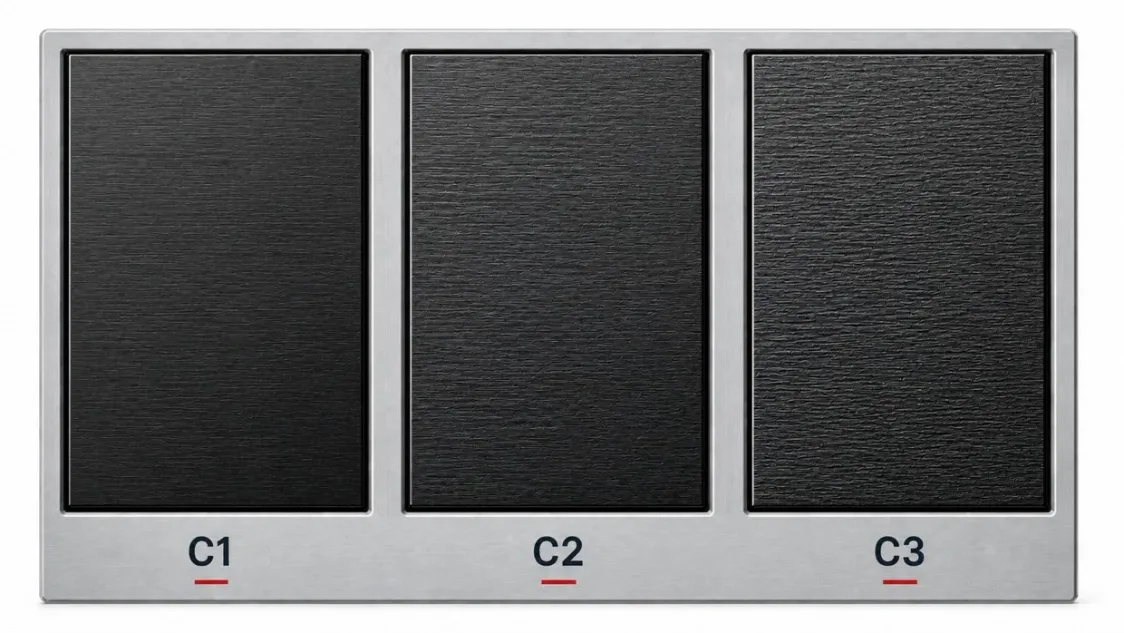
SPI C
Ra 0.28 – 0.55 µmLow-gloss to matte finishes that cut glare and hide flow lines
| Grade | Ra (µm) | Method | Best for |
|---|---|---|---|
| C1 | 0.28 – 0.35 | #600 stone | Non-reflective functional parts |
| C2 | 0.35 – 0.40 | #400 stone | Grippy tools & housings |
| C3 | 0.40 – 0.55 | #320 stone | Internal / non-cosmetic parts |
SPI D
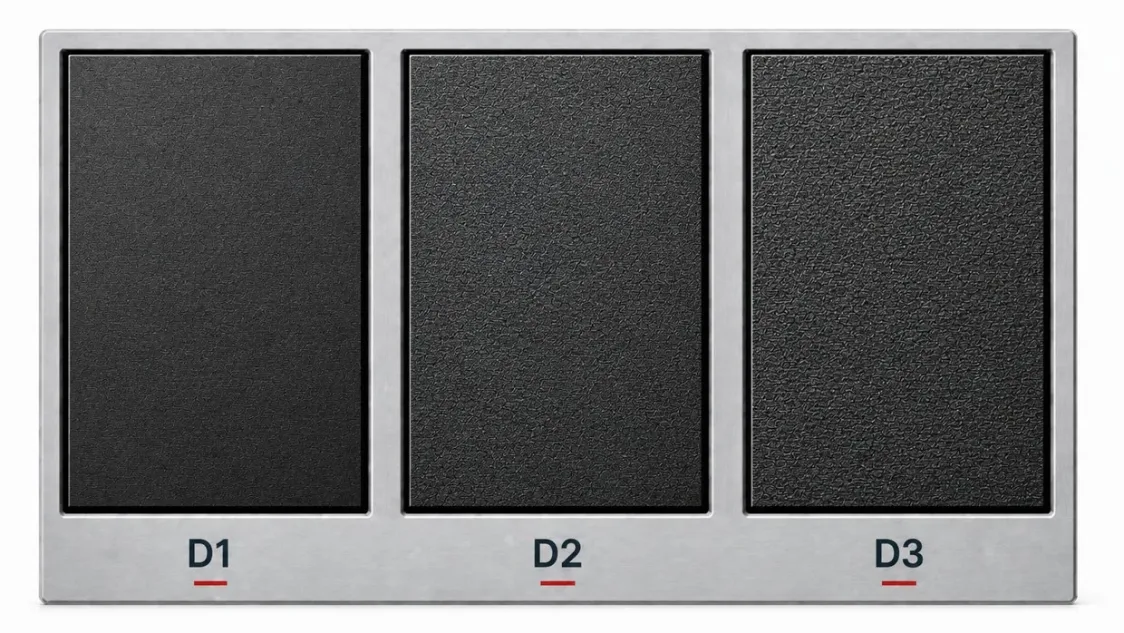
Ra 0.55 – 1.50 µmTextured matte finishes built for grip and concealment
| Grade | Ra (µm) | Method | Best for |
|---|---|---|---|
| D1 | 0.55 – 0.80 | #11 bead blast | Tactile, non-slip grips |
| D2 | 0.80 – 1.00 | #240 oxide blast | Hides molding & ejector marks |
| D3 | 1.00 – 1.50 | #24 oxide blast | Heavy-duty; anti-glare textures |
How HM Manufacturing’s Injection Molding Process Works
From your first online quote to final delivery, HM Manufacturing runs one connected injection molding process. A single project team, fewer handoffs and clear visibility at every step keep your project on spec, on budget and on time
/01
Upload Design File
Start by uploading your 3D CAD files and 2D drawings to HM Manufacturing, setting the stage for precise custom molding
/02
Get Quote with DFM
Select materials, surface finishes and shipping options. Receive an injection molding quote and manufacturability feedback within one business day
/03
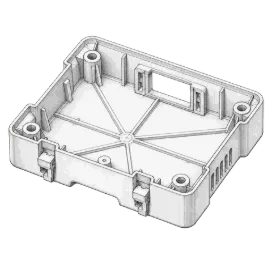
Review T1 Sample
We produce a T1 sample for your approval. Check every detail against your specifications. Qualifying projects can reach T1 in as fast as two weeks
T1 REVIEW
/04
Production Begins
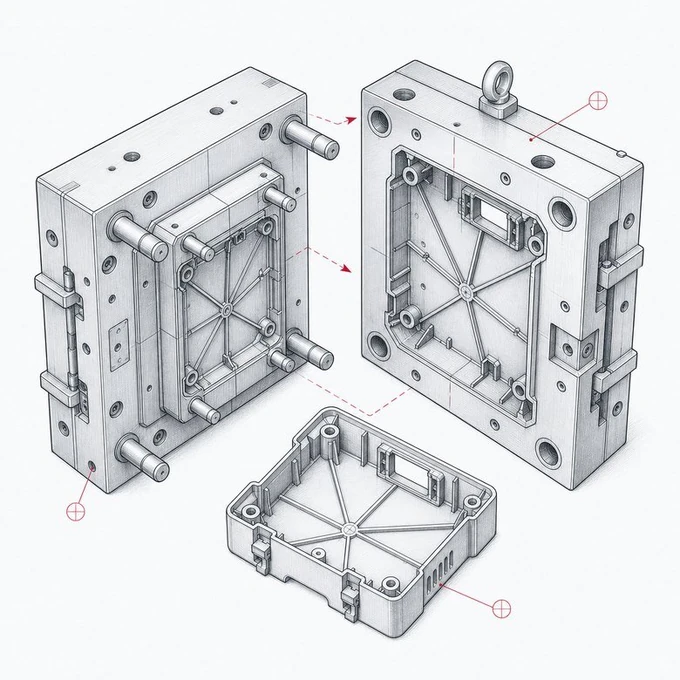
After sample approval, we move into full-scale production while maintaining agreed quality and dimensional requirements
/05
Delivery
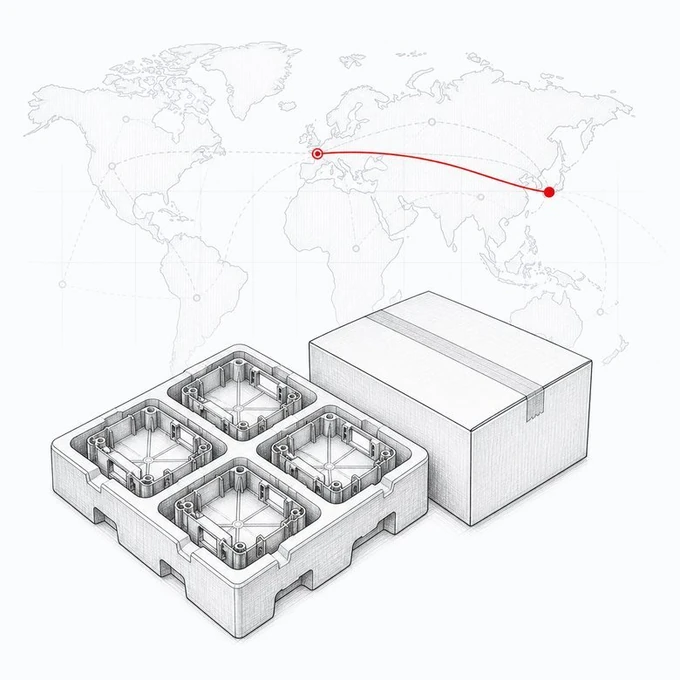
We ship custom injection molded parts to 120+ countries, with delivery available within seven days after production release
/06
Ready to Start
Start your injection molding project with HM Manufacturing. Move from DFM review to tooling, production and delivery with one project team
Precision Injection Molding Quality Control & Compliance
At HM Manufacturing, quality is controlled at the mold design stage. It starts with a DFM review, where our engineers settle wall thickness, gate location and shrinkage before any steel is cut. Communication stays efficient and transparent through the whole project. Cavity tolerances are held within ±0.02 mm and molding tolerances within 0.03-0.05 mm, under ISO 9001 certified processes. More than 70% of our clients choose to work with us again
Advanced Inspection Equipment
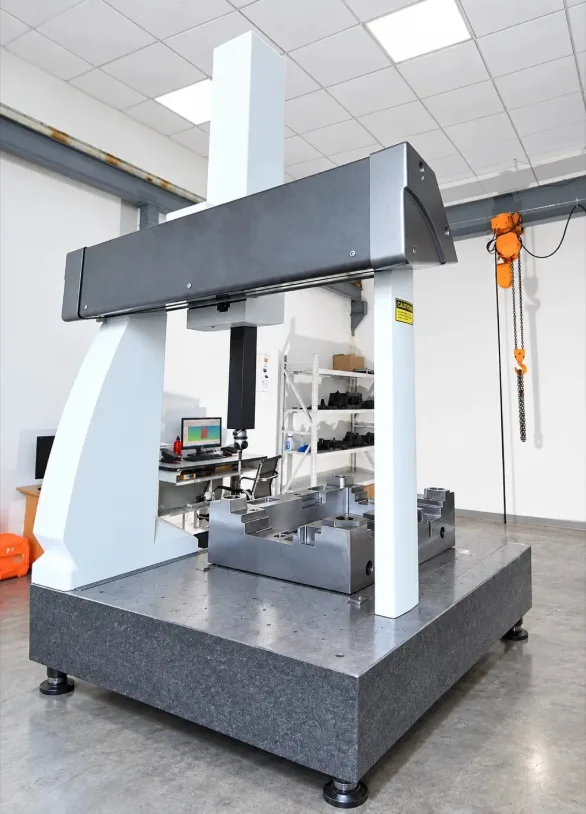
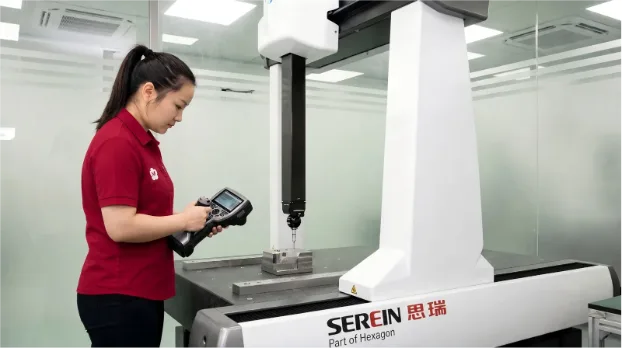
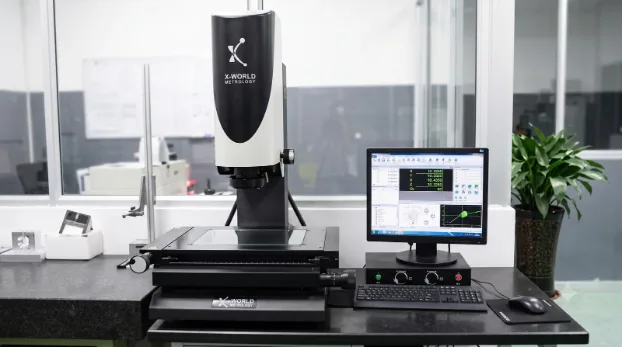
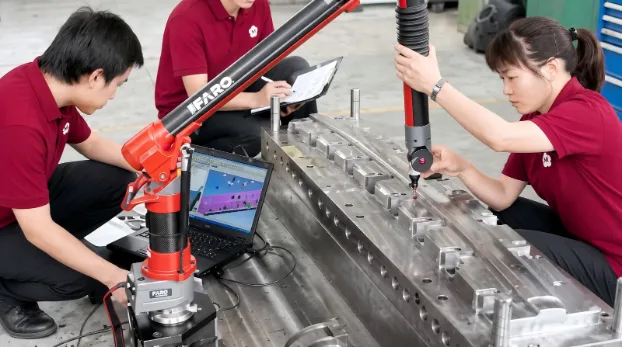
We use CMM, 2D vision measuring systems, portable measuring arms, height gauges, micrometers and calipers to check part dimensions, mold cavity dimensions and surface finish, holding molding tolerances at 0.03 to 0.05 mm and cavity tolerances within ±0.02 mm
Comprehensive Inspection Documentation
We provide detailed inspection reports such as first article inspection (FAI), dimensional measurement reports, material certificates, RoHS and REACH test reports, and pre-shipment inspection records to support your quality management
Certified Manufacturing Partner
Holding certifications including ISO 9001, IATF 16949, ISO 14001, LFGB, FDA and BSCI, HM Manufacturing is a trusted partner for industries with strict quality requirements such as automotive, medical devices, consumer electronics and e-commerce brands
Injection Molding Project Examples by Industry
HM Manufacturing partners with brands across the medical, automotive, electronics, industrial and robotics sectors. From first-time innovators to global enterprises, we deliver precision injection molding trusted for quality, reliability and consistent performance worldwide
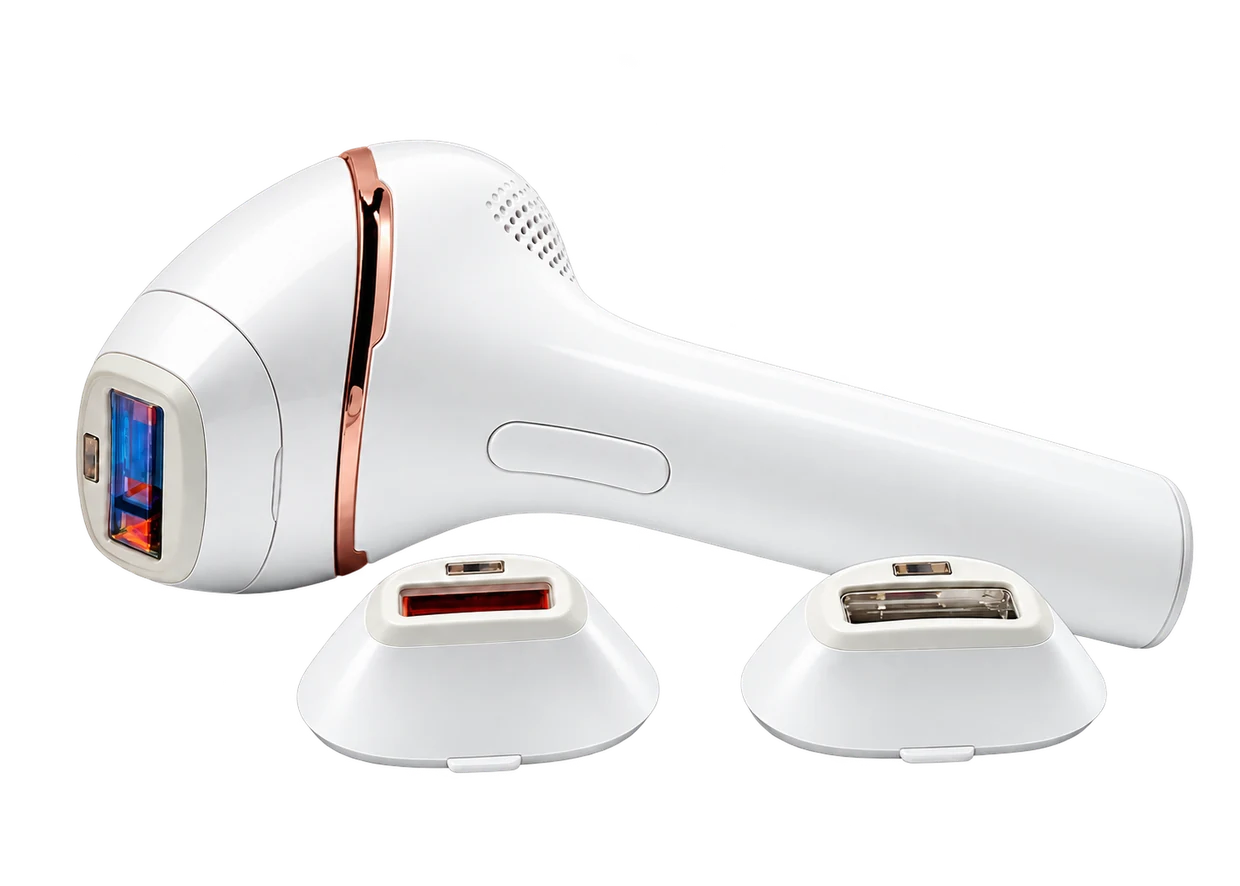
Portable Beauty Device: From Product Concept to Retail-Ready Production
A brand needs a visually consistent handheld product without committing to excessive opening inventory. The project framework combines prototype verification, housing DFM, cosmetic surface planning, production molding and final packaging through one coordinated path
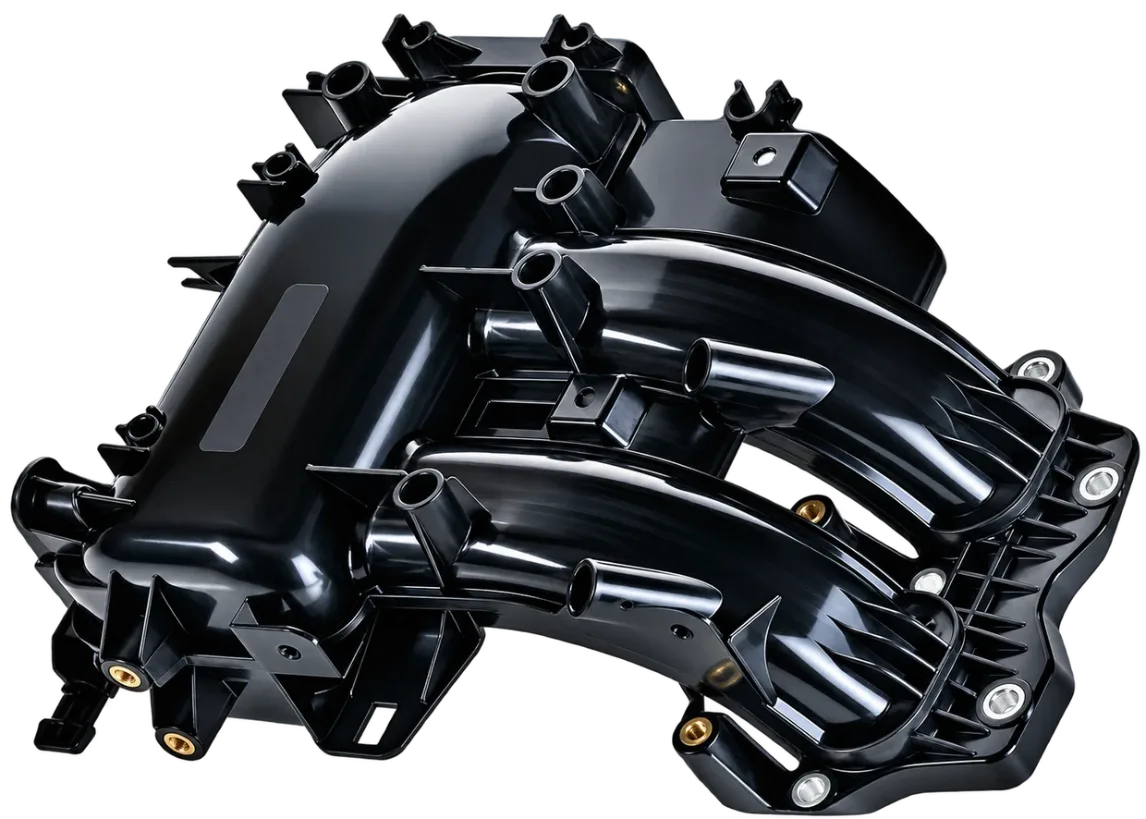
Structural Interior Bracket: From Load Requirements to Repeatable Molding
An automotive component must balance strength, dimensional stability and controlled assembly interfaces. The project framework aligns engineering resin selection, rib and boss design, tooling strategy, trial validation and dimensional inspection before production release
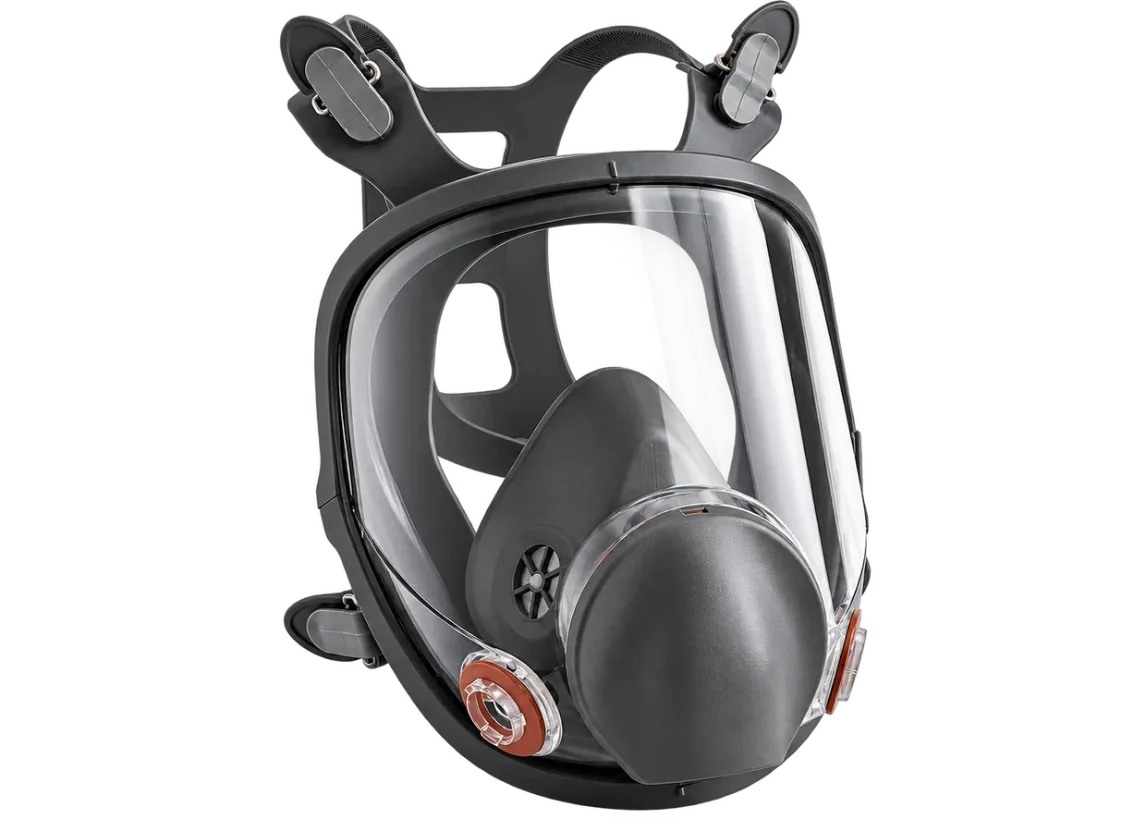
Clear Device Housing: From Material Review to Controlled Production
A visible medical-device housing requires clear material documentation, controlled cosmetic surfaces and stable fit between molded components. The project framework connects drawing review, resin confirmation, mold polishing, first-part inspection and project-specific reporting
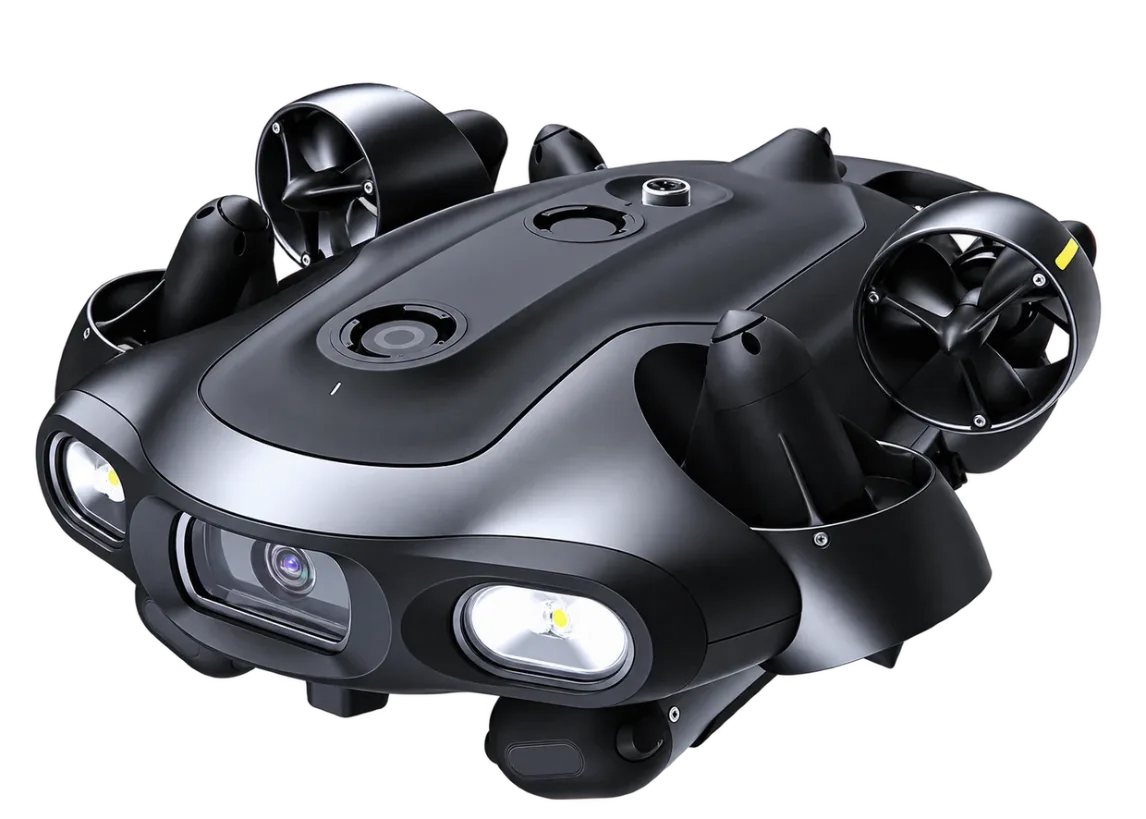
Multi-Part Electronics Enclosure: From Fit Verification to Surface Finish
A compact electronics enclosure needs reliable part fit, controlled wall thickness and consistent visible surfaces. The project framework connects prototype verification, mold design, injection molding, decoration planning and assembly review before production approval
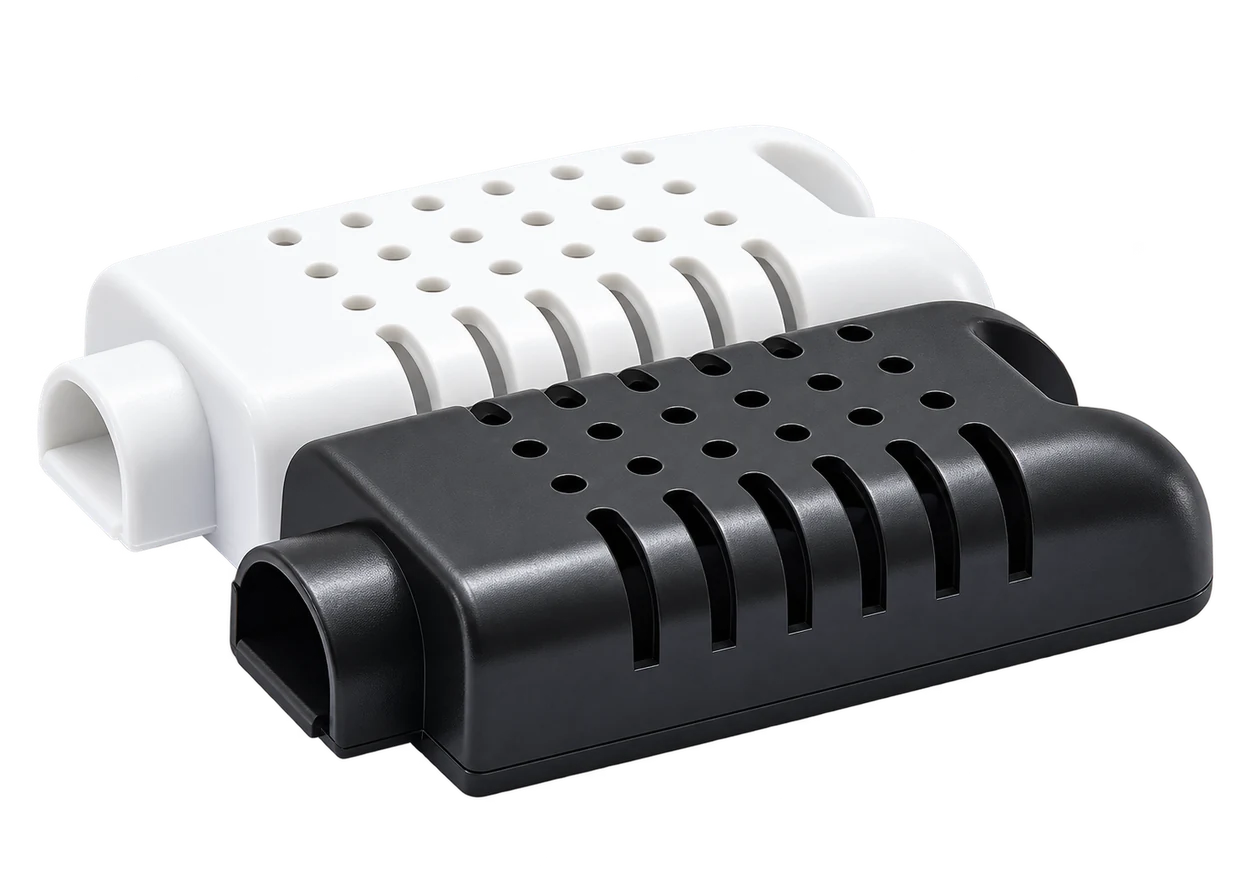
Lightweight Sensor Housing: From Geometry Review to Precision Molding
A lightweight sensor housing requires disciplined control of critical interfaces, wall transitions and inspection dimensions. The project framework combines drawing review, material selection, mold-cavity control, first-part verification and documented dimensional checks
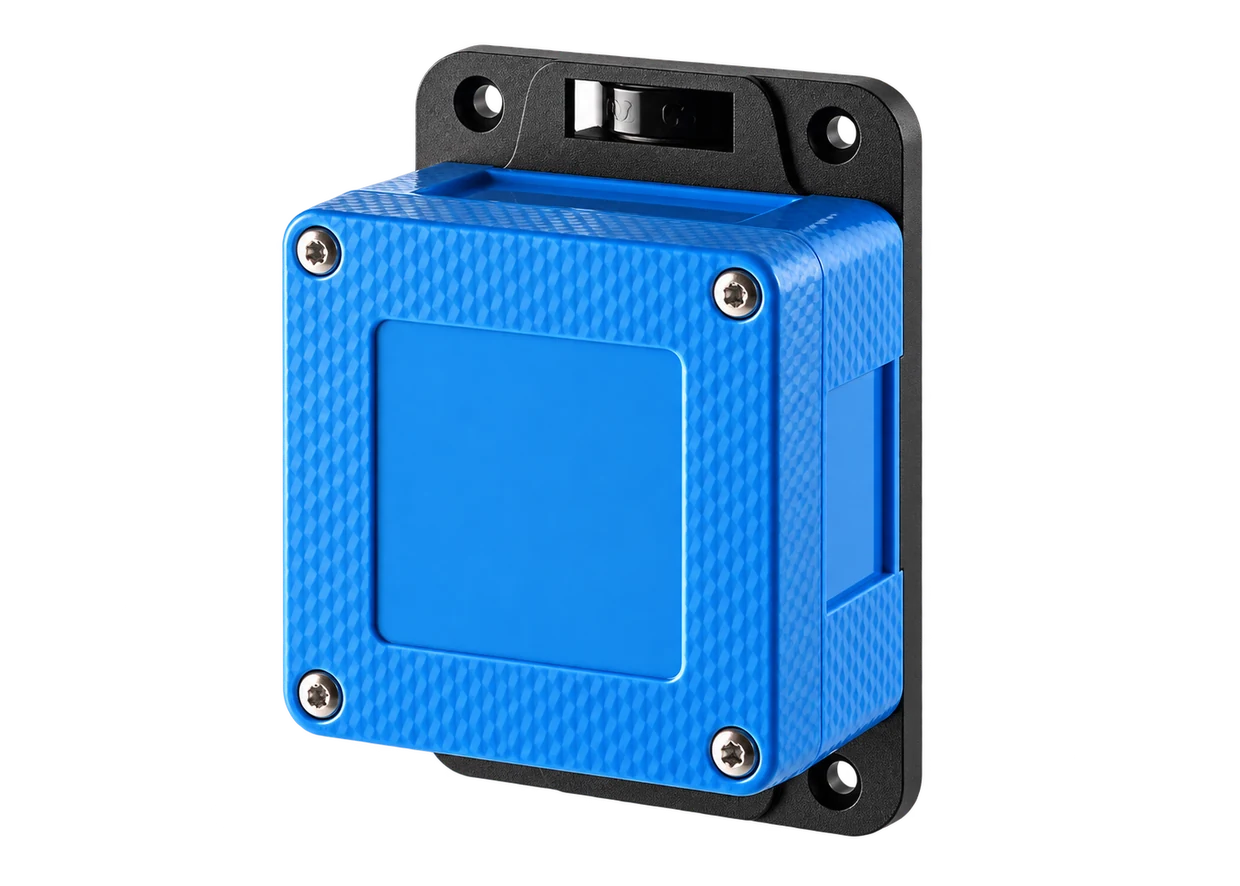
Industrial Control Housing: From Material Selection to Finished Assembly
An industrial control housing must protect internal components while supporting stable mounting and service access. The project framework coordinates resin selection, structural DFM, mold development, molding, secondary operations and final inspection
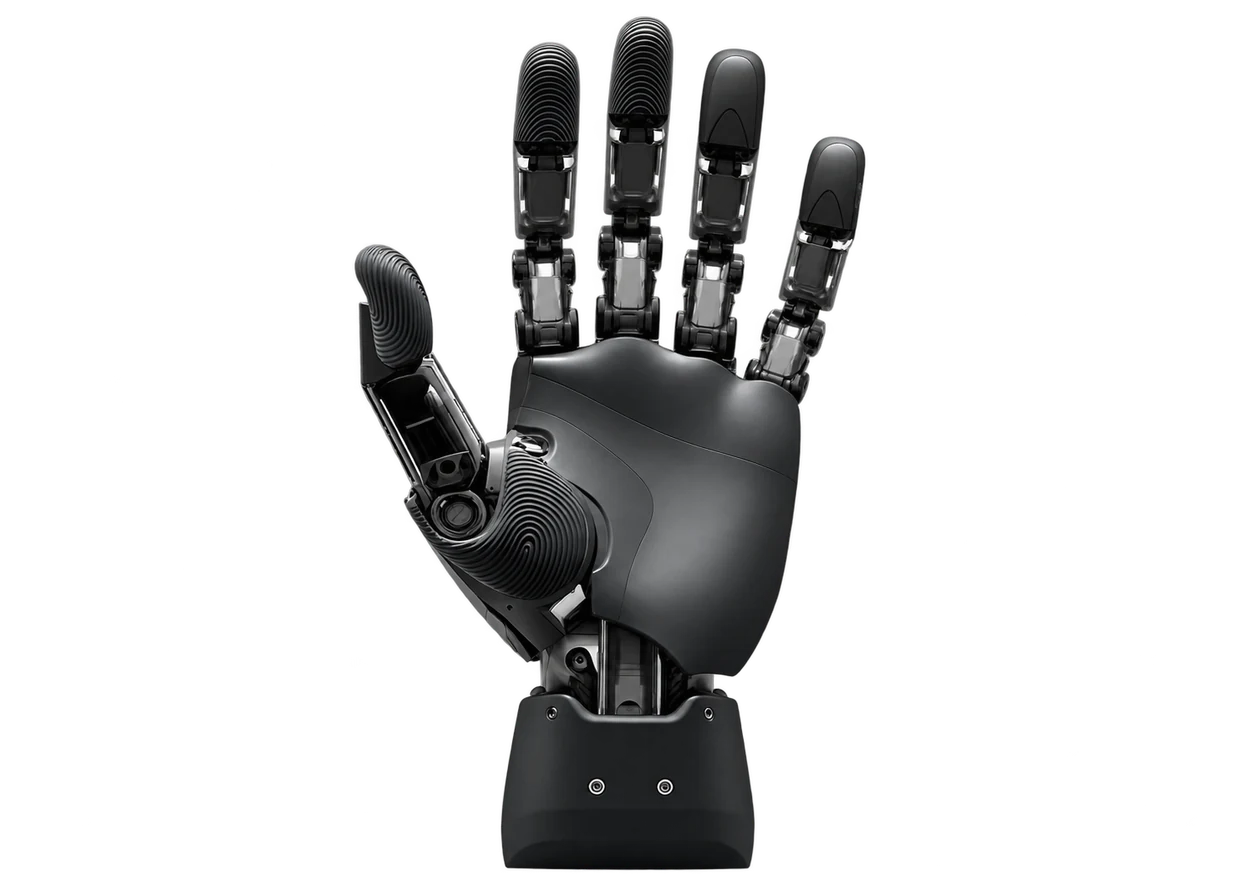
Robot Sensor Cover: From Fast Prototype to Production Tooling
A robot-mounted sensor cover needs early confirmation of clearances, fastening features and cable interfaces. The project framework uses rapid prototype verification before steel tooling, followed by molded-part inspection and assembly-fit review
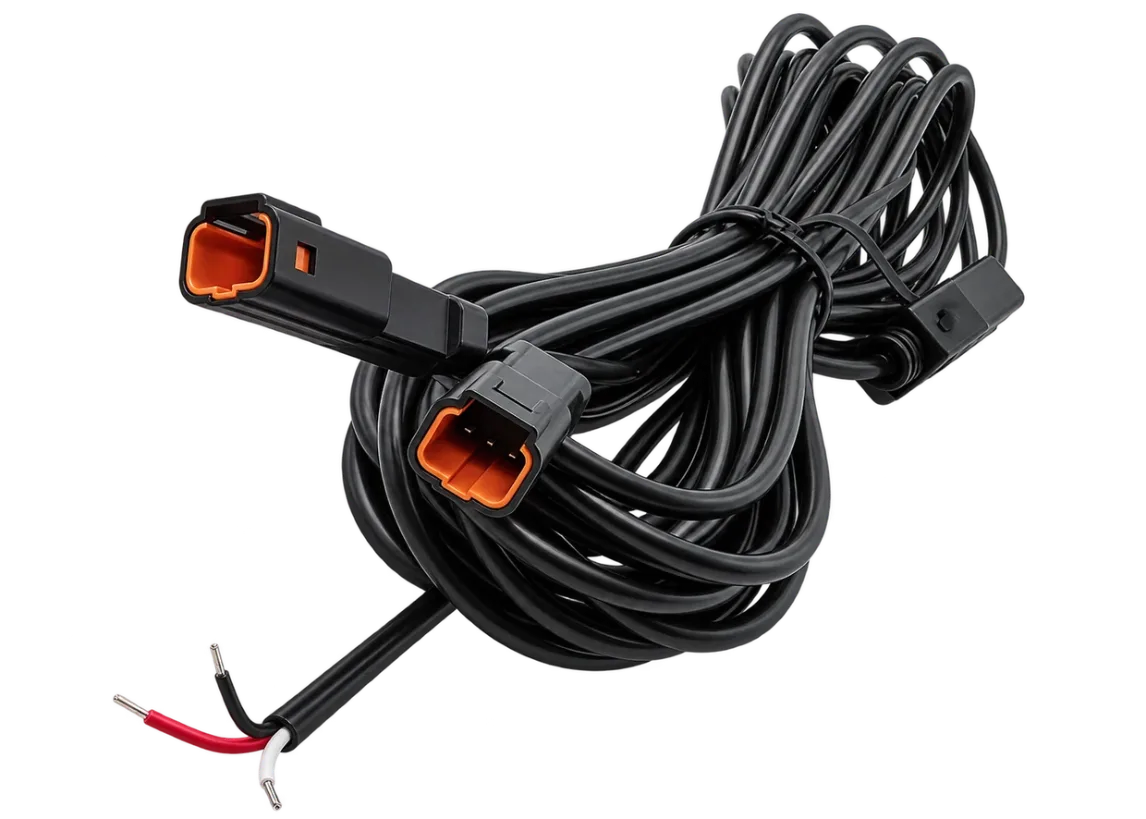
Power Connector Housing: From Interface Review to Production Molding
A power connector housing requires controlled mating geometry, stable wall sections and a production plan matched to expected volume. The project framework links DFM, tooling, molding parameters, dimensional checks and coordinated delivery
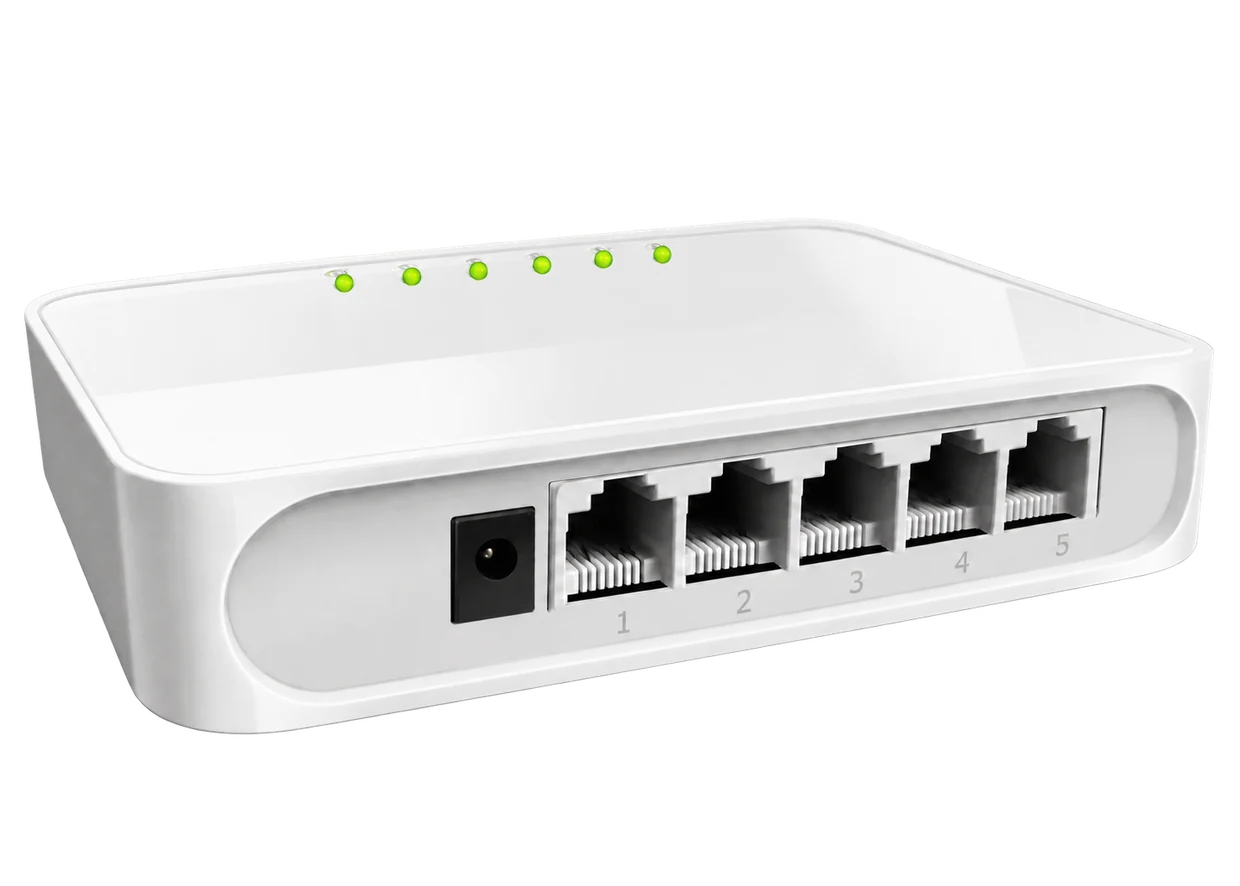
Communication Equipment Enclosure: From Detail Design to Repeatable Assembly
A communication enclosure must control internal component fit, external appearance and repeatable assembly interfaces. The project framework combines drawing review, mold design, injection molding, surface treatment planning and final-fit inspection
Your Custom Injection Molding Manufacturer in China
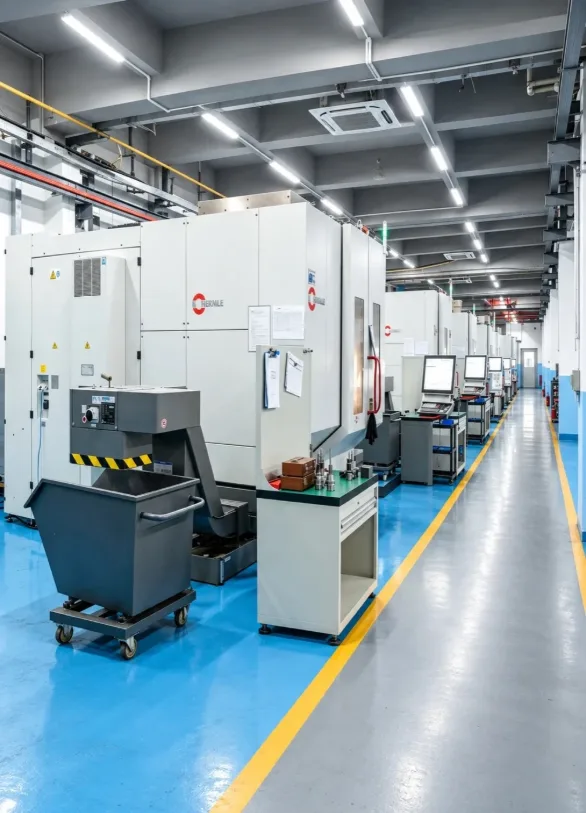
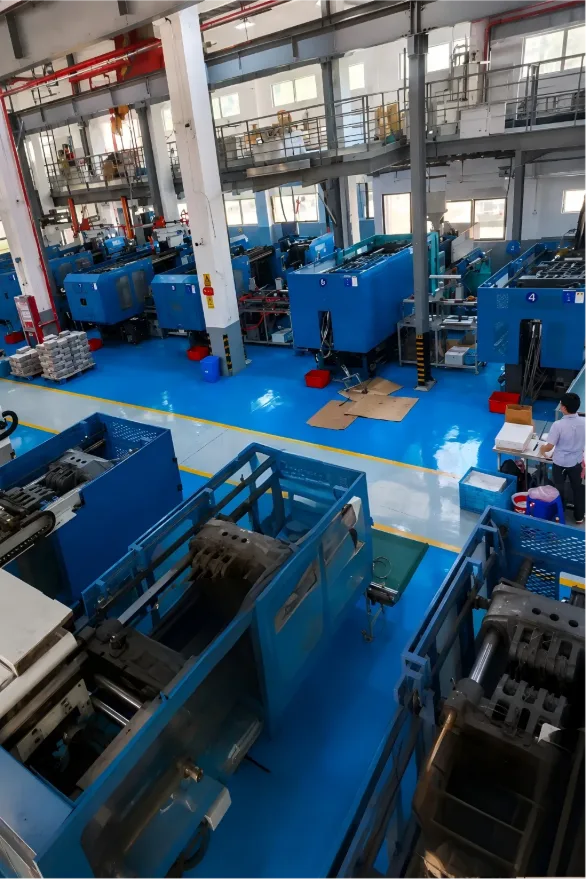
HM Manufacturing is headquartered in Taizhou, China, with mold making and injection molding run in our own factory and backed by a vetted network of 500+ partner factories across China, delivering high-quality, on-demand manufacturing for custom plastic parts. As your strategic partner, we ship to North America, Europe and beyond, with 3D-printed samples ready in as fast as 3 days. Our English-speaking project team keeps communication clear across time zones, so your production stays efficient, reliable and on schedule